What Materials Can a Fiber Laser Cut? A Practical List of Yes, Conditional, and Never
First, Confirm the Type of Fiber Laser You Are Evaluating A compatibility chart may group steel, ABS, polycarbonate, and composites…

A guy walked into my shop last week, proud as a peacock because he’d bought a “pro” laser for $450 on an auction site. He had an order for 200 custom wedding invites, and he’d calculated that at $5 apiece, he could pay off the machine in a single weekend. He was looking at the sticker price—but he wasn’t looking at the clock.
By Saturday night, he was back in my lobby, nearly in tears. It wasn’t that the machine didn’t work; it was that it worked exactly as advertised. He’d discovered that “cutting” and “production” are two different languages, and his cheap machine spoke with a stutter. He ended up refunding the client and walking away with a $450 lesson because his “bargain” was earning him less than a dollar an hour. He hadn’t bought a business; he’d bought a bottleneck.

A $500 diode laser and a $5,000 CO2 laser can both technically cut through a sheet of 3mm plywood, but the diode might do it at 300 millimeters per minute while the CO2 hums along at 1,800. If you’re a hobbyist making one keychain for your nephew, that 15-minute difference is just a cup of coffee. If you’re running a small batch of fifty units, that difference becomes 10 hours of your life you aren’t getting back.
In a production environment, your “cost” isn’t just the material; it’s the shop rate. If you value your time at a modest $40 an hour, a machine that takes an extra 20 minutes per job is charging you a $13.33 “labor tax” every time you hit the start button. Over a hundred parts, you’ve just “spent” $1,333 in lost time—more than the price difference for a better machine. You’re not saving money; you’re financing a slow machine with your own sweat equity at a predatory interest rate.
The bottleneck usually hides in the power density and the motion system. Budget machines often use “gantry-style” frames with rubber wheels on aluminum extrusions, which vibrate like a tuning fork if you try to push them beyond a crawl. To get a clean cut, you have to slow down even further. You end up babysitting a machine that moves at the speed of a tectonic plate, unable to start the next job because you’re stuck waiting for the current one to finish its fifth pass.
So what happens when that slow machine finally runs into a hard deadline it can’t possibly meet?
Cheap machines are built on the “hope” method of engineering: they hope you won’t run them for eight hours straight. To hit a sub-$1,000 price point, manufacturers swap industrial-grade components for consumer-grade junk. Instead of a sealed RF (radio frequency) laser source that lasts for years, you get a glass DC tube that requires a literal bucket of water and a fish-tank pump for cooling. If that $20 pump fails while you’re mid-cut on a deadline, the heat buildup can crack your $500 laser tube in seconds.
When a component fails on a budget rig, you don’t just lose the cost of the part; you lose the “trust equity” you’ve built with customers. I’ve seen people lose $2,000 contracts because a $5 plastic stepper motor driver overheated and fried on a Thursday night, and the replacement had to arrive by slow boat from overseas. A professional machine uses standard, over-spec’d electronics designed to dissipate heat. They’re built for a 100% duty cycle, meaning they don’t need a “nap” between jobs to avoid melting their own brains.
Production is about predictability. If you can’t guarantee that the machine will fire tomorrow morning, you can’t build a business; you’re just gambling with a high-voltage light bulb. The real cost of a cheap machine shows up the moment you have to tell a client their order is late because your “bargain” decided to smoke a capacitor.
But even if the machine stays powered on, can it still produce identical parts by the end of the day?
The first part off a cheap laser usually looks good enough to fool you. But watch what happens by part number 100. Budget machines typically use thin-gauge sheet metal, or even acrylic, for their frames, held together by friction and a few bolts. As the machine moves, it generates kinetic energy. Over hours of operation, those vibrations slowly rattle the fasteners loose or, worse, cause the frame to “settle” into a slightly different shape.
In fabrication, we call this precision decay. If your frame isn’t rigid, your circles start looking like eggs, and your squares won’t sit flush when you try to assemble them. That forces you to increase the “tolerance” in your designs, which means you can’t nest parts tightly together on a sheet of material. If you have to leave a 5mm gap between parts because your machine’s accuracy is wandering, you’re wasting 15% more material than the person with a rigid machine who can nest parts 1mm apart.
Material waste is a silent profit killer. If you’re burning through $500 of material a month, a 15% waste factor is $75 out the window every 30 days. Over two years, that’s $1,800 in the trash—again, almost exactly the price difference between a flimsy hobby rig and a real piece of equipment. You end up paying for the expensive machine anyway through wasted wood and acrylic; you just don’t get the benefit of owning it.
How does this mechanical instability affect the actual software workflow and your ability to scale?
Try pointing a high-end 20W diode laser at a piece of clear acrylic, and you’ll learn a $400 lesson in physics: the beam passes straight through the plastic without leaving a mark. It isn’t a matter of power or quality; the material is simply “transparent” to the 450nm wavelength that blue-light diodes use. To that laser, the acrylic isn’t even there.
Photons from different laser sources vibrate at specific frequencies, and materials absorb energy only when that “frequency” matches their molecular structure. CO2 lasers operate at a 10.6µm wavelength, which organic materials like wood, leather, and most plastics absorb greedily. Fiber lasers live at 1.06µm, a frequency that resonates perfectly with the crystalline structure of metals but bounces off wood like a rubber ball.
This isn’t a software setting you can adjust or a “hack” you can dig up on a forum.
If your business plan depends on cutting clear signage or thick architectural models, a $1,000 diode rig is little more than a paperweight. You’re pushed into the $5,000 to $10,000 CO2 bracket before you’ve even cut your first part. Conversely, if you want to mark stainless steel tumblers without messy chemical sprays, a CO2 laser is the wrong tool; you need the $30,000 entry-level fiber machine.
The material chooses the tool. You’re just the one who has to sign the check.
But what happens when the wavelength is right, yet the “punch” behind the beam is lacking?
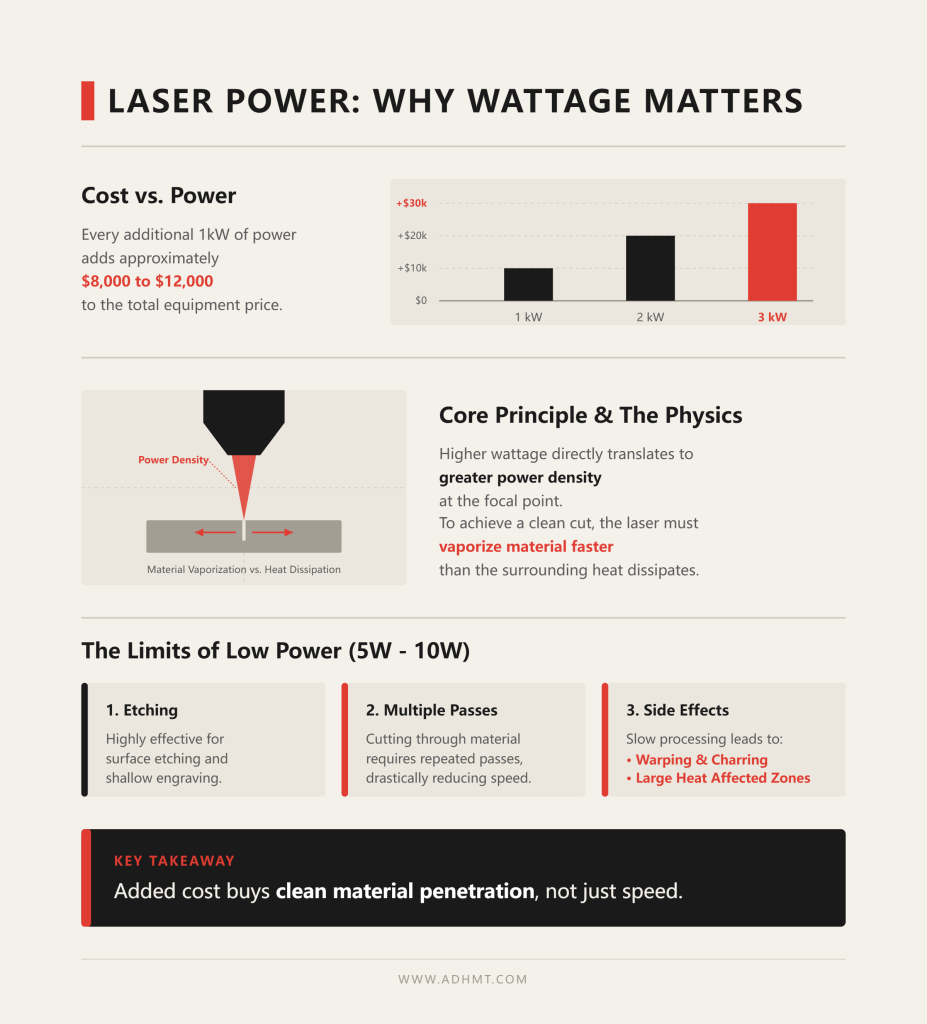
Every additional kilowatt of power on an industrial fiber laser adds roughly $8,000 to $12,000 to the sticker price. That isn’t a “speed tax” designed to gouge the impatient; it’s a physical requirement for piercing thicker material. When a laser hits a material, it must melt and vaporize the substrate faster than the surrounding area can absorb and carry the heat away.
Think of it like trying to boil a pot of water with a single match. You can hold that match there all day, but you’ll never reach a boil because the water dissipates heat faster than the match can supply it. In the same way, a 40W CO2 laser will never cleanly cut 1-inch-thick timber, no matter how slowly you run it. The beam loses focus and the heat spreads sideways, charring the edges into a charcoal mess before it ever reaches the bottom of the cut.
Higher wattage enables greater “power density” at the focal point.
If you’re looking at a $500 machine, you’re likely getting 5W or 10W of output. That’s enough to etch a logo, but the moment you try to cut 1/4″ plywood in a single pass, the machine hits a wall. You end up running four or five passes, which increases the “heat affected zone,” warps your material, and ruins the precision of your fit.
You aren’t just paying for speed; you’re paying for the ability to penetrate the material without burning the house down.
Does that mean the cheapest machine in the right category is always the logical starting point?
Buying a laser that is “almost” right for your material is the fastest way to pour capital down the drain. Beginners often fall into the trap of buying a $600 diode laser because it claims it can “mark metal,” only to discover that it requires a $50 bottle of ceramic marking spray and three minutes of prep time per part. In a small-batch run of 100 parts, that adds up to 300 minutes of manual labor that a fiber laser would have eliminated immediately; for shops moving toward metal-focused production, ADH Machine Tool’s dual-use fiber laser cutting machine is a more relevant bridge because it sits within a CNC-based laser cutting and sheet metal automation portfolio built for production work rather than improvised diode workflows.
The machine becomes a bottleneck not because it is broken, but because it is fundamentally mismatched to the job.
A “bargain” that cannot perform your business’s primary task is not an asset; it is a liability that consumes floor space and mental energy. If you buy a CO2 laser to cut thin copper shims because it was $20,000 cheaper than a fiber laser, you will find that the copper reflects the beam back into the laser head, shattering your expensive optics. You did not save $20,000; you spent $10,000 on a machine that will destroy itself the moment it tries to do its job.
The value of a laser is binary: it either processes your specific material palette at a profitable rate, or it does not.
Once you accept that physics dictates the machine type, the question shifts from “What’s the cheapest?” to “What is the minimum viable specification that can actually fulfill an order?” That reality pushes you away from the Wild West of the hobbyist market and into the three hard-edged price tiers that define the industry.
So how do these technical requirements translate into the actual price tags you will see on the market?
If you have accepted that your material dictates the laser source, you have already avoided the most expensive mistake in fabrication. Now you face the reality of the market: three distinct price brackets that may appear to offer similar specs, yet behave like entirely different species of machine.
For readers comparing those brackets against real production needs, ADH Machine Tool’s CNC-focused laser cutting and sheet metal automation portfolio can be a useful reference point; you can download the brochure and technical materials to review concrete machine options before weighing price against capacity.
Buying a laser is not like buying a car, where a more expensive model simply comes with nicer seats and a better stereo.
In the shop, price tiers represent a shift in who is doing the work. In the low tier, you are the machine’s servant, constantly tweaking, squaring, and troubleshooting. In the high tier, the machine becomes your employee: reliable, predictable, and almost invisible.
The price tag is simply a down payment on how much of your own time you are willing to sacrifice.
This is the realm of the “open frame” machine: a laser head mounted on aluminum extrusions, with little else included. For a hobbyist making Christmas ornaments for family, these can feel like a miracle of modern engineering. For someone trying to run a business, they are a siren song leading straight into a swamp of hidden costs.
You see a $600 price tag and think you’ve won. Then you realize you need a $300 enclosure to keep smoke out of your lungs, a $200 air-assist pump to prevent wood from charring, and a $150 honeycomb bed so your parts don’t weld themselves to your workbench.
By the time the machine is actually production-ready, you’ve spent $1,500—and you still have a machine that moves at a crawl.
Diode lasers are inherently slow because they rely on “blue light” technology, which lacks the raw thermal punch of CO2. To cut 1/4-inch plywood, you might need three passes at 100mm/minute. If you’re making 50 widgets, you’ll be sitting there all night watching a blue light flicker while your hourly profit margin evaporates.
If you value your time at $40 an hour, the “cheap” diode can become the most expensive tool in your shop within the first month.
This is where the “silent partner” begins to take shape. In this bracket, you stop buying “parts” and start buying a “system.” These machines are almost always enclosed, with built-in exhaust ports, lid safety sensors, and integrated cooling systems that help prevent the laser tube from overheating and cracking.
The most critical upgrade in this tier isn’t the laser itself, but the brain inside the box.
Most machines in this range use industry-standard controllers, such as the Ruida system, which allows you to run professional-grade software like LightBurn. This isn’t a minor detail; it’s the difference between wrestling with a proprietary app that crashes every time you import a complex file and a workflow where you hit “send” and the machine simply executes.
In a small-batch environment, you need to trust that the 50th part will look exactly like the first.
Because these are CO2 machines, they move significantly faster than diodes—often five to ten times faster for cutting operations. You’re paying for the ability to turn a four-hour job into a forty-minute job. This is the “sweet spot” because it offers the strongest ROI for a solo operator: the machine is fast enough to keep up with orders, but it doesn’t require the $50,000 capital investment of a full industrial rig.
Does a faster machine automatically mean more profit, or is another bottleneck hiding in the physical dimensions of the work area?
At the $8,000 mark and beyond, you are no longer paying for more “features”; you are paying for “uptime.” These machines are built with components designed to run eight hours a day, five days a week, for years. They replace inexpensive glass laser tubes—consumables that fail after 1,000 to 2,000 hours—with ceramic or metal RF (Radio Frequency) tubes that can last a decade and be recharged.
An industrial machine does not just move fast; it moves with “positional accuracy.”
Cheap machines use rubber belts that stretch over time, producing circles that look like ovals and joints that no longer fit. Industrial rigs use high-end linear rails and servo motors that can “talk back” to the computer, ensuring the laser head is exactly where it is supposed to be, even at high speeds. This eliminates the “rework tax”—the cost of throwing away ruined material because the machine skipped a beat. For shops ready to move from troubleshooting to repeatable production, ADH Machine Tool’s CNC-based laser cutting range offers a practical next step with a precision laser cutting machine built around accuracy, automation, and industrial throughput.
You are buying a utility, like the electricity in your walls.
When you flip the switch on an $11,000 Trotec or Epilog, you know it is going to work. You are not checking the water level in a bucket or tightening belts. You are simply feeding it material and taking out finished product. For a shop with a backlog of orders, the cost of the machine being “down” for a single day is higher than the monthly payment on the equipment.
Buying industrial-grade speed is a wasted investment if a cramped work area turns you into a full-time material handler while your margins disappear into a pile of un-nestable scrap.
A standard 4×8-foot sheet of Baltic Birch plywood yields 32 squares if your laser bed is a measly 12×12 inches, which means you must handle that material 32 separate times just to process one sheet. Every time the laser stops, you have to walk over, open the lid, clear the scrap, load the next piece, and find your zero point. If that cycle takes just two minutes, you have burned more than an hour of your life on a single sheet of wood before the laser has even fired its first pulse. In a fabrication shop, the machine should be working for you; with a small bed, you are working for the machine.
Larger beds—specifically those that can accommodate a 24×36-inch “quarter sheet” or a 24×48-inch “half sheet”—transform the geometry of your workday. When you can nest 50 parts onto a single large board, you create a “set-it-and-forget-it” window. That sixty-minute cut cycle becomes an hour you can spend finishing parts, responding to customer emails, or quoting the next job. The machine is effectively paying your salary while you do other things.
Small beds also impose a “scrap tax” on every job. You can rarely fit parts perfectly into a 12-inch square, which creates awkward offcuts that are too small to use but too big to throw away. A large bed enables “nesting,” allowing small parts to fill the gaps between larger parts and squeeze every cent of value from the raw material. If you can increase your material yield from 70% to 90% simply by having a larger workspace, the machine can pay for the price difference in bed size within its first year of operation.
How do you turn that physical workspace into actual cuts without spending hours dragging icons around a computer screen?
Proprietary software bundled with “bargain” lasers is often little more than a glorified printer driver, and it can choke on complex vector files. I’ve seen beginners waste entire mornings trying to “clean up” a DXF file because their cheap software couldn’t handle more than 500 nodes without crashing. Professional control systems—most notably those built on Ruida or Trocen hardware and paired with LightBurn—treat the laser like a precision CNC tool rather than a desktop printer.
That distinction matters because of “Boolean operations” and “array tools.” In professional software, you can take a single earring design and, with three clicks, fill an entire 20×28-inch sheet with 200 perfectly spaced copies to minimize wasted wood. If you have to do that manually in a clunky, basic interface, you’re not a fabricator; you’re a data-entry clerk. High-end software also supports “layer logic,” where the machine knows to engrave the fine details first, then cut the inner holes, and finally cut the outer perimeter—preventing parts from shifting or falling out of focus mid-job.
Cheap controllers also lack “true path optimization.” A smart controller calculates the most efficient route for the laser head, minimizing “dry fire” time when the head is moving but not cutting. On a complex sheet of 100 parts, a smart path can reduce total run time by 15%. Over a week of production, that adds up to hours of “found time” that simply don’t exist on a machine running an entry-level GRBL board or a locked proprietary app.
If the software handles the logic, how do you handle the physical reality of placing the material in the right spot every single time?
Setting the “Z-height”—the distance between the lens and the material—is the most frequent task you will perform, and doing it manually with a plastic “focus spacer” invites inconsistency. If the wood has a slight warp or you are a millimeter off with your manual gauge, the cut line widens, the wood chars, and the part goes into the trash. Auto-focus sensors, whether they use a physical probe or an ultrasonic trigger, remove the “human variable” by hitting the exact focal point every time you swap materials.
Modern production rigs take this a step further with “camera-aided positioning.” Instead of “eyeballing” where your design will land on a piece of scrap wood, an overhead camera shows you the live bed on your computer screen. You simply drag the digital design over the physical scrap, and you’re ready to cut. Without this, you can spend ten minutes per job “dry running” the laser with the red-dot pointer to make sure you are not about to cut into thin air.
These seconds of setup time are the “friction” that prevents a business from scaling. A machine with auto-focus, a camera, and a reliable home-positioning system can be ready to fire in under thirty seconds. A “cheap” machine requires a ritual of measuring, jogging the head, and test-firing that can take five to ten minutes per sheet. When you are running ten sheets a day, that is nearly two hours of setup time that provides zero value to your customer.
Even if you solve the material-flow problem, a machine that produces parts at this speed creates a major secondary challenge: a cloud of toxic smoke and a layer of soot that will destroy your optics if you did not budget for air management.
A laser is a controlled fire. When you cut material, you are not simply “removing” it; you are vaporizing it into a cocktail of fine particulates and toxic gases. Cutting acrylic releases sweet-smelling but headache-inducing fumes, while MDF off-gasses formaldehyde and glue resins that can coat your lungs as effectively as they coat your shop walls. The tiny 40mm “muffin fans” included with entry-level machines are toys. If you can smell the laser from the next room, you are failing the most basic requirement of industrial production. For buyers comparing open-frame equipment with safer, production-minded options, ADH Machine Tool’s CNC laser range makes a covered system such as a dual-use fiber laser cutting machine with cover a more relevant next step than another under-ventilated hobby machine.
To run a business, you need a high-static-pressure blower or a multi-stage HEPA filtration unit. A real extraction system moves air fast enough to create a vacuum seal on the cabinet, ensuring that no “leakage” enters your workspace. This is not just about comfort. If soot lingers in the cabinet, it settles on your rails, gums up your bearings, and forces the motor to work harder, eventually causing skipped steps and ruined parts.
This is where the “cheap” laser’s sticker price starts to fall apart. A professional-grade fume extractor, such as a BOFA unit, can cost $1,500—often more than the beginner laser itself. You can try venting out a window with a $200 inline fan, but your neighbors may eventually call the fire department once your shop starts smelling like a burning plastic factory. Poor air management does not merely annoy the neighbors; it creates a film of grime on the very components that make the laser work.
Active cooling is the single most important factor in machine longevity. Beginners often start with a five-gallon bucket of water and a pond pump, which is a disaster for production: as the water warms, the laser’s efficiency drops and the tube comes under stress. A refrigerated industrial chiller—a real one, like a CW-5200—is a non-negotiable $550 expense that keeps your beam stable and your tube alive for years. Without it, you are effectively burning through $300 replacement glass tubes every six months because you did not want to buy the proper radiator.
This maintenance deficit compounds at the nozzle. Without a steady stream of high-pressure air assist, smoke bakes onto the optics, creating permanent opaque spots that crack the $120 zinc-selenide lens and foul the mirrors. You might save a grand on the initial purchase, but you will pay it back in $400 increments every time inadequate cooling or dirty air assist forces an emergency overhaul of your optical path.
When these components inevitably fail under deadline pressure, who do you call to get back online?
The “11 PM Rule” is simple: when your machine dies in the middle of a rush order at 11 PM on a Tuesday, how long does it take to find a fix? If you bought a generic import, your “support” is a translated PDF and a Facebook group. In a production environment, every hour the laser sits idle is a direct hit to your reputation. If your Ruida controller board fries or a specific Y-axis stepper driver burns out, you are not just one phone call away from a solution. On a cheap import, that specific proprietary component is coming from a warehouse in Shenzhen. Even with “express” shipping, you are looking at 14 to 21 days with a dead machine while your customers move to the competitor down the street who can actually meet a deadline.
Professional brands command a premium because they keep parts stocked in your country and employ technicians who actually answer the phone. If a critical component fails, a reputable vendor can have a replacement on your doorstep by noon the next day. That reliability is what separates a minor hiccup from a business-ending catastrophe. Beginners often overlook the cost of “lost opportunity.” If you lose a $2,000 contract because your machine is waiting on a slow boat from China, that “cheap” laser has just become the most expensive tool in your shop. You are not just buying a box of parts; you are buying a relationship with a supply chain that keeps your business breathing.
If you are comparing suppliers on more than sticker price, it is worth asking how the machine, support model, and upgrade path fit your real production mix. ADH Machine Tool’s CNC-based portfolio spans laser cutting and broader sheet metal automation, making a supplier evaluation discussion a practical next step before committing capital.
A service bureau quote of $2.50 per part looks expensive until you realize it includes the operator’s salary, electricity, and insurance you have not paid for yet. When you outsource to a shop running $300,000 fiber lasers, you are renting world-class precision and speed without the headaches of maintenance or capital risk. For a beginner, the most dangerous move is “buying the job”—purchasing a machine for a single contract without calculating whether your labor on a slower, cheaper machine will consume the profit the service bureau was already preserving for you.
Owning the means of production only makes sense when your “burdened” cost per part—raw material plus your hourly labor, electricity, and the machine’s depreciation—falls significantly below the outsource price. If a local shop charges you a $2.00 markup and you can cut the same part yourself for $0.50 in “total burden,” you are “earning” $1.50 per part. To justify a $10,000 entry-level professional setup, you need enough volume to recover that $10,000 in $1.50 increments before the machine needs its first major overhaul.
The math changes the moment your “cheap” machine forces you to perform manual work that a professional machine would automate. If you spend twenty minutes cleaning soot off parts because your air assist is weak, or ten minutes per sheet hand-nesting because your software is basic, your labor cost skyrockets. You might save $5,000 on the sticker price, but if you spend an extra five hours a week on “non-value-added” labor, you have effectively taken a pay cut to become a full-time janitor for your own machine.
How do you make sure the machine you buy today does not become a boat anchor the moment your business actually starts to succeed?
Buying a laser with a 12″ x 20″ bed because it fits your current product is a classic “ceiling” mistake. In small-batch production, your biggest overhead is not the laser tube; it is the “setup time”—the minutes spent loading material, homing the head, and pressing start. A machine that fits four units per sheet requires four times the loading and unloading labor of a machine that fits sixteen. By spending 30% more upfront for a larger bed, you can often cut your daily labor hours in half by letting the machine run longer unattended.
Power works the same way: a 40W laser that can “technically” cut 1/4″ plywood is still a production bottleneck. It forces you to crawl at 2mm per second, which chars the edges and increases the likelihood of a fire. Stepping up to an 80W or 100W tube lets you triple your travel speed on that same material, which does more than increase output—it improves part quality by reducing the “heat-affected zone.” A machine that is “too powerful” for your daily needs can always be turned down, but a weak machine will always leave you waiting.
Upgrading a machine is far more expensive than buying the right one the first time. You lose money on the resale of the old unit, lose production time during the transition, and have to learn the quirks of a new controller and software all over again. If your business plan projects even a 20% growth rate, buying a machine that is currently running at 50% capacity gives you the buffer to scale without requiring a major capital injection six months later.
If the goal is to move from being a “hobbyist with a side hustle” to operating like a manufacturer, where do you draw the line between a budget-friendly starter machine and an industrial workhorse?
To find your floor, apply the “Hardest-Highest” rule: your machine must be over-spec’d for your hardest material and built to handle your highest projected monthly volume. If you buy for today’s smallest job, you effectively cap your company’s growth at its current infancy.
| Hardest Material | Monthly Unit Volume | Minimum Viable Tier | Realistic Payback Window |
|---|---|---|---|
| Paper, Leather, <1/8″ Ply | <50 units | Enclosed Prosumer Diode/CO2 ($1k–$3k) | 3–6 Months |
| 1/4″ Acrylic or Plywood | 50–250 units | Mid-Range CO2 + Dedicated Chiller ($4k–$8k) | 6–12 Months |
| 3/8″ Acrylic or Hardwoods | 250+ units | Professional CO2 / RF Tube Source ($10k–$18k) | 12–18 Months |
Do not view these tiers as “good, better, best.” View them as “survivability ratings.” A $2,000 hobbyist machine tasked with cutting 200 sheets of acrylic a month will not just be slow—it will vibrate itself out of alignment or burn through its cooling system before it ever pays for itself.
The “Part-Cost Paradox” is the final hurdle: if you cannot prove that your machine saves more in labor hours than it costs in monthly financing or capital outlay, you have not bought a tool—you have bought a second job that pays less than minimum wage. Your objective is not to find the cheapest machine that “can” cut; it is to find the most affordable machine that lets you stop working on the laser and start working on the business. Choose the tool that makes your time worth $100 an hour, not the one that keeps you chained to the shop floor for $10.
