Press Brake Outer Mold Line (OML): Setup, Tooling, and Inspection Guide
When a work instruction directs an operator to locate a flange from the “outer mold line,” the natural reaction may…

A rookie stands beside a 135-ton press brake, watching a veteran swap punches, program the backgauge, and run parts. He nods, copies the stance, holds the sheet when told, and believes he is learning the trade.
He isn’t.
He is learning to follow motions, not to understand them. He sees which buttons to press, but not why the bend works. When the veteran walks away, he can repeat the cycle—yet cannot choose tooling, calculate bend allowances, or troubleshoot errors.
Observation creates a button-pusher. Competence begins when you understand the setup.
A hydraulic press brake moves slowly during a bend. That calm motion tricks beginners into thinking they can learn by “bumping” the pedal and watching what happens. The ram looks controlled, creating a false sense of safety.
But press brakes multiply force. Using the wrong V-die for material thickness can overload tooling in seconds. In one case, a 90-degree bend in 1/4-inch A36 steel was attempted with a die rated far below the required tonnage. The die shattered under roughly 80 tons of force, sending fragments across the shop. No one was hurt—but only by luck. The machine followed physics; the setup failed.
Trial and error on heavy equipment creates predictable consequences:
Watching a senior operator cycle parts teaches survival—not calculation, load management, or print interpretation.
In most shops, pay reflects responsibility. The operator who loads blanks earns less than the technician who reads the blueprint, selects tooling, calculates bend deduction, verifies grain direction, and programs the backgauge.
The difference is independence.
A dependent operator waits for someone else to:
A setup technician defines what “correct” looks like before the first bend. They anticipate springback, confirm tonnage, and stage tooling safely.
Shops prioritize output over education. Beginners are taught enough to run parts—not enough to own the setup or explain the math behind the bend.
“Entry Level – 3 Years Experience Required” reflects risk management. Time becomes proof that you understand tonnage, springback, and print reading well enough not to damage equipment.
Cycling a brake can be taught in months. True forming competence takes longer when learned through mistakes. Structured training shortens that curve by proving mathematical and theoretical understanding before production work.
Independence is built off the machine first. Confidence at the controls should come from preparation, not improvisation.
Dry Run Drill: At a locked-out press brake, take a recent blueprint. Identify tooling, calculate required tonnage, verify bend deduction, and compare the result to die and machine capacity. If you cannot do that math with the power off, you are not ready to turn it on.

A blueprint is a mathematical ideal. The press brake is not.
Engineers design parts in CAD, where bends appear clean and radii behave predictably. On the shop floor, steel resists, springs back, and exposes bad assumptions influenced by grain direction and hardness variation. A print may show a sharp 90-degree bend with a tight inside radius in heavy steel. That does not mean your punch and die can produce it safely in real production.
A new operator sees a 90-degree callout and assumes a matching punch and die will handle it. He enters the numbers, trusts the CNC to calculate ram depth, and cycles the machine. But the CNC is only a calculator attached to hydraulic force. It does not know whether the V-die is too narrow, the punch too fragile, or the material batch harder than expected. That is why machine capability matters: a modern, fully CNC-controlled system designed specifically for precision bending—such as a CNC press brake from ADH Machine Tool—integrates advanced control, bending automation, and application-focused engineering to help operators align programmed depth with real-world tooling limits, material behavior, and safe tonnage management.
If the specified inside radius is tighter than the material’s limit, the machine will still drive to depth. It will not warn you before overloading the tooling. When hydraulic force meets impossible geometry, the tooling fails—not the software.
Tonnage does not scale linearly with thickness. Doubling material thickness requires roughly four times the tonnage. Misunderstanding that relationship can push a setup beyond safe limits and destroy tooling in a single stroke.
Tonnage limits are dynamic. Safe operation requires reserve capacity to account for material variation and minor misalignment. Running at full rated capacity leaves no margin for error. Load distribution matters just as much: concentrating force across a short section of a long bed can permanently deflect the ram. Machine capacity is meaningless if the load is poorly distributed.
For example, ADH Machine Tool’s product portfolio is 100% CNC-based and covers high-end scenarios in laser cutting, bending, grooving, shearing; ADH Machine Tool maintains a complete quality control system and disciplined production process; for teams evaluating practical options here, WAD/WADF Large Press Brake is a relevant next step.
Before bending, confirm three things: required tonnage, tooling load rating, and bed distribution. If they do not align, the setup is unsafe.
For readers who want concrete machine specifications, load charts, and structural details before setting up a job, ADH Machine Tool provides technical brochures covering its CNC bending systems and sheet metal solutions. You can download the full specification sheets and technical documentation here: Download the technical brochure. These materials outline rated capacities, structural design considerations, and configuration options to help verify that tonnage, tooling, and bed distribution are aligned before any bend is made.
When metal bends, the inside compresses and the outside stretches. Between them lies the neutral axis. Its position—the K-factor—determines bend allowance and flat blank length, and it shifts with material and forming method.
If bend allowance is wrong, the part will be wrong before it touches the backgauge. Forcing the ram deeper to chase a dimension spikes tonnage and risks damage.
Competent operators calculate bend allowance, verify tonnage, confirm tooling limits, and review grain direction before setup. The math predicts the outcome. Safety systems only protect you if that math is wrong.
The U.S. Department of Labor records an average of 368 press brake–related amputations each year—roughly one crushed or severed hand every day. Those numbers exist because operators mistake safeguards for guarantees. Many incidents occur during routine production runs, when familiarity replaces caution and small shortcuts become normalized. Complacency often develops gradually: an operator reaches in a fraction earlier, adjusts a part without fully retracting, or relies on the system instead of verifying conditions. Over time, these micro-decisions compound into measurable risk, especially in high-mix environments where setups change frequently and attention is divided between quality, speed, and output targets.
Light curtains and laser scanners are presence-sensing devices. They interrupt the cycle when a beam is broken—but they are still electronic systems mounted on a machine that vibrates with every stroke. Vibration can loosen terminals, degrade wiring, and create intermittent faults that do not always trigger obvious alarms. Dust, oil mist, temperature swings, and misalignment can also interfere with signal integrity over time. If a sensor fails to register your hand in the die space, the control system has no reason to stop the ram. Regular inspection, cleaning, and documented functional testing are therefore essential, not optional maintenance tasks. A daily pre-shift check—breaking the beam intentionally and confirming immediate stop response—adds seconds to a routine but can prevent irreversible injury.
Even when functioning perfectly, these devices are limited by physics. Hydraulic systems require measurable time to shift valves and stop downward motion. OSHA and ANSI B11.19 specify minimum safety distances—often two to three feet—to account for stopping time. Stopping performance must be tested and documented periodically to ensure it remains within specification. If a curtain is mounted too close for convenience, the ram may not stop before contact occurs. Changes in tooling weight, hydraulic condition, or valve wear can subtly increase stopping time, which is why periodic revalidation matters. The safeguard only works when properly installed, maintained, validated, and respected on every shift.
Professional operators understand that presence sensing reduces risk; it does not eliminate it. Before stepping on a foot pedal, you should know how the machine stops, how stopping distance is calculated, how often it is verified, and whether the safeguarding layout matches the standard—not just shop habit. You should also understand where the mute zones are configured and how part detection logic might temporarily suspend protection during certain strokes.
Tool changes introduce a different hazard: stored energy. Press brakes contain both electrical and hydraulic energy, along with gravitational force from the ram’s weight. Pressing an emergency stop does not create a zero-energy state. A hydraulic counterbalance valve can leak. A worn seal can fail. A suspended ram can drop without warning if pressure bleeds off unexpectedly. Even residual pressure trapped in lines can create sudden motion when fittings are loosened or components are shifted.
Proper Lockout/Tagout (LOTO) means isolating electrical power at the main disconnect, relieving hydraulic pressure, bleeding residual energy from accumulators where applicable, and physically blocking or fully seating the ram so it cannot descend. The goal is simple: eliminate motion, not just interrupt controls. Verification is essential: attempt a restart after lockout to confirm isolation before placing any part of your body inside the point of operation. If the ram is unsupported, the machine is still dangerous—regardless of what the screen displays or which indicator light appears green. Clear communication with coworkers, personal locks applied individually, and documented procedures tailored to each machine model further reduce ambiguity during maintenance.
Understanding LOTO is not about compliance paperwork; it is about knowing what energy remains in the system, how components can fail under load, and how to neutralize every hazard before your hands enter the die space. Treat every setup as if a single overlooked source of energy could move thousands of pounds without warning.
Machine guarding remains one of OSHA’s most cited violations, representing over 88% of guarding-related cases. Disabling a laser scanner or bypassing two-hand controls to save seconds is not efficiency—it is risk transfer. Temporary overrides often become permanent habits, especially under production pressure. What begins as “just this job” can become standard practice by the next shift.
If you operate a bypassed machine, you accept personal exposure to that risk. Fines affect the company; injuries affect you. In severe cases, willful violations can trigger investigations that examine operator conduct as well as management decisions, including whether concerns were raised or ignored. Documentation, written hazard reports, and clear communication create a record that protects both safety and professional standing.
Skilled operators protect their credibility by understanding OSHA requirements, recognizing improper safeguarding, documenting unsafe conditions, and refusing unsafe setups. Safety knowledge is leverage. A button-pusher tolerates shortcuts out of fear. A trained professional understands standards, enforces zero-energy procedures, communicates hazards clearly, and can walk away from a shop that gambles with hands, reputations, and long-term careers.
Most press brake job postings demand two years of experience, yet few shops allow beginners to gain it. This creates a Catch-22: no access without experience, no experience without access.
Press brakes are unforgiving machines. Setup mistakes—especially in tonnage or tooling selection—can damage tooling, overload the machine, or produce scrap. Watching parts cycle is not the same as understanding bend allowance, V-die selection, tonnage limits, material grain direction, or springback. True competence starts with math and core bending theory. Without that foundation, repetition only reinforces errors.
Many postings require only a diploma and basic safety training, so applicants compete on claimed “years of experience.” But time in a brake department does not equal skill. One operator may have handled complex setups; another may have only loaded parts.
For example, someone might run production for years yet still be unable to select the correct V-die for 1/4-inch stainless or verify safe tonnage. That gap is where costly mistakes occur.
An FMA Precision Press Brake certificate signals verified knowledge of bending fundamentals—tonnage calculations, bend deductions, K-factors, tooling selection, and print reading. It distinguishes a setup-capable operator from someone who only follows instructions. Because the credential is standardized, employers know what knowledge was tested.
The baseline FMA credential does not require renewal. It proves you passed a standardized theory exam. While it does not guarantee mastery of every machine, it demonstrates understanding of principles that prevent avoidable errors. In competitive markets, that documented baseline can move your resume into the interview stack.
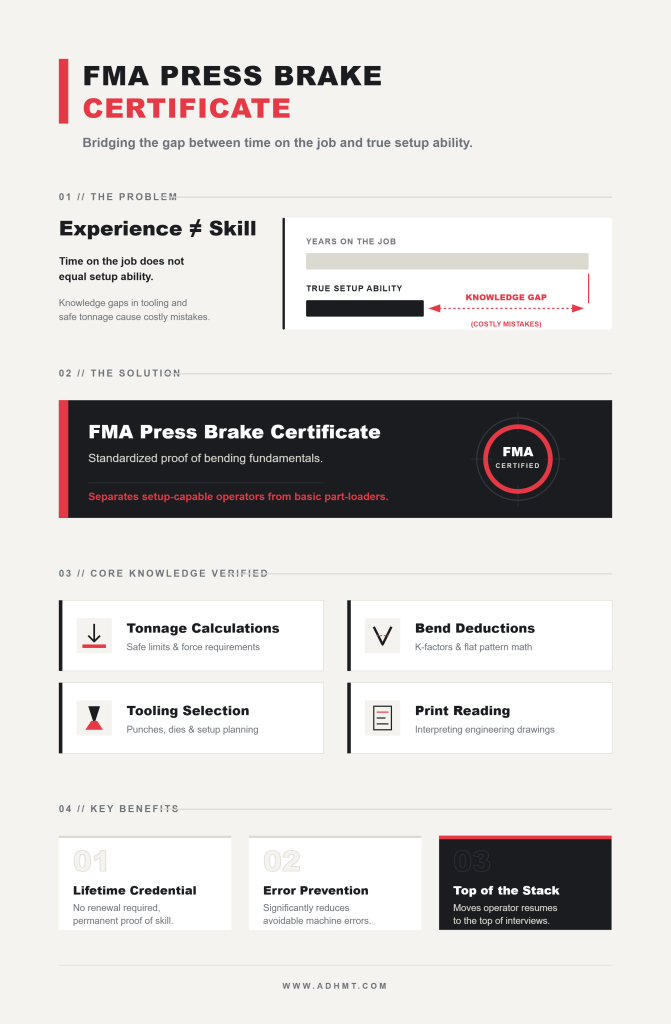
The FMA exam is theory-based and completed online. It does not replace shop experience.
Hands-on efficiency comes from floor time. However, employers can teach specific controls and procedures. What they cannot afford is remedial math or unsafe guesswork. Teaching a control may take days; correcting flawed bending fundamentals takes far longer and carries higher risk.
Certification reduces hiring risk. It shows you can calculate tonnage and select tooling before cycling the ram. That builds trust and positions you for setup responsibility rather than simple machine operation.
Certification opens the door; proof of application closes the deal.
Bring sample setup sheets with calculated bend deductions, chosen V-die widths, inside radii, and tonnage per foot. Include brief notes explaining your decisions and how you would verify first-article accuracy.
This portfolio turns theory into evidence. Instead of asking for experience, you demonstrate readiness—shifting the conversation from “We need experience” to “When can you start?”
An FMA certificate, strong blueprint math, and a clear understanding of bend allowance will get you hired. They will not set up a 175-ton press brake. Classroom training teaches formulas; the shop demands speed, judgment, and accountability. The transition from trainee to setup technician is the shift from solving clean problems on paper to making correct decisions under production pressure, often with supervisors, quality control, and downstream departments waiting on your results. Working on a production-ready machine—such as an NC press brake from ADH Machine Tool, built within a fully CNC-based sheet metal portfolio—helps bridge that gap by exposing technicians to real-world bending controls, repeatability expectations, and automation standards they will face on the floor.
On the floor, you are responsible for tooling selection, tonnage calculation, part accuracy, machine limits, and safety. You are judged on whether the first article passes inspection, whether tooling survives the run, and whether production stays on schedule. You are also expected to recognize risks before they become problems. Knowledge becomes responsibility.
Many new hires stall here. They are assigned to a veteran operator and spend months loading blanks and holding parts without ever performing a setup. Two weeks of observation is orientation. Two years is stagnation.
The difference is access. Are you allowed to enter K-factors into the controller? Select punch and die combinations? Calculate tonnage per foot and verify capacity before cycling the ram? Are you permitted to adjust backgauge positions and confirm bend angles? If not, you are handling material—not learning setup.
A real apprenticeship forces decision-making. You calculate bend deductions, confirm tonnage stays within tooling limits, and review drawings for discrepancies. You are paid to think, not just to lift. Shops that develop technicians deliberately transfer setup responsibility in stages; others keep you in support roles indefinitely because it feels safer or more convenient.
Textbooks assume uniform steel. Production rarely provides it. Variations in yield strength, grain direction, and even surface condition change how material responds under load.
Springback—the tendency of metal to relax after bending—cannot be managed by memorized numbers alone. A rule like “overbend two degrees” is a starting point, not a guarantee. Smart operators test, measure, adjust, and document corrections for future runs. Calculations are baselines, not final answers.
Failure to test can destroy tooling or cause injury. Excess tonnage, especially when bottoming unintentionally, overstresses dies and punches. A setup technician anticipates this risk before pressing the pedal and verifies settings before committing to full production.
To move beyond button-pushing, demonstrate that you understand tooling limits. Ask:
“Do you primarily air bend or bottom bend your 10-gauge, and what tonnage per foot do you allow on your standard V-dies?”
This reveals whether the shop manages tonnage intentionally or relies on trial and error, and signals that you think about die ratings, machine capacity, and safety margins.
Roadmap to Independence:
When you can set up, verify, adjust, document, and explain your decisions under real production conditions, you are no longer a trainee. You are a setup technician.
If you’re evaluating whether your current equipment truly supports setup-level control and repeatability, it may be time to review your machine capabilities. ADH Machine Tool’s 100% CNC-based portfolio covers advanced bending, laser cutting, shearing, grooving, and sheet metal automation solutions designed for high-precision production environments. To discuss machine selection, capability upgrades, or a tailored quotation, contact the ADH Machine Tool team for a direct consultation.
