Press Brake Outer Mold Line (OML): Setup, Tooling, and Inspection Guide
When a work instruction directs an operator to locate a flange from the “outer mold line,” the natural reaction may…

In my years investigating amputations, I have seen more severed fingers on press brakes equipped with “plug-and-play” light curtains than on machines with no guarding at all. Shop owners watch an operator sweep a hand through the invisible field to stop the ram mid-stroke, nod in satisfaction, and wrongly believe they have bought OSHA compliance for $3,000. Bolting a light curtain onto a press brake does not guarantee safety—it creates a deadly illusion. True OSHA compliance requires mathematically tying the safe distance to the machine’s stopping time, verifying control reliability, and rigorously eliminating shop-floor workarounds.
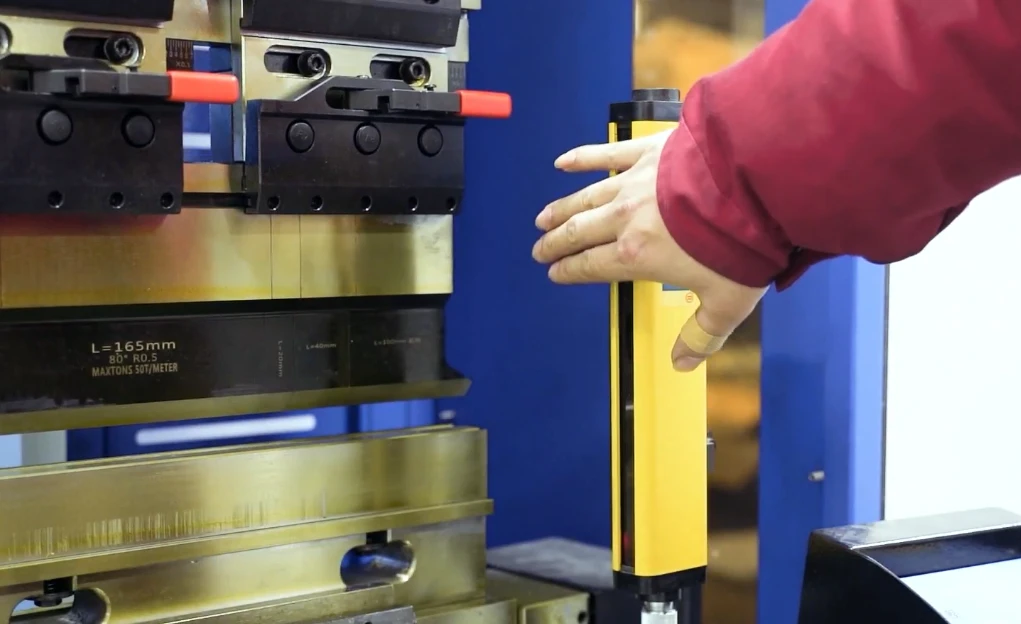
Waving a hand through the beam proves exactly two things: the wiring has continuity, and the relay clicked. It tells you nothing about how long it takes that massive steel ram to actually stop its downward motion.
Press brakes are kinetic monsters. When the beam is broken, an electrical signal travels to the machine control, which tells the hydraulic valves to dump pressure, which eventually starves the cylinders and stops the die. That mechanical sequence takes milliseconds. But human hands move at 63 inches per second. If your curtain is mounted four inches from the pinch point, and your aging brake takes a quarter-second to stop, the operator’s fingers are already crushed before the hydraulics even begin to respond.
Think of the light curtain not as a protective shield, but as a tripwire. A tripwire does not stop the enemy; it only triggers the alarm. If the alarm sounds but the blast doors take too long to close, the tripwire is useless. So what happens when an operator trusts a tripwire that the machine cannot support?
In OSHRC Decision TMD 17-05601, a fabrication facility faced a $12,675 penalty for operating press brakes with no guarding at all. Its defense was painfully common: it assumed its experienced operators knew better than to put their hands in the die. That assumption is dangerous, but relying on an uncalibrated light curtain is worse.
OSHA penalty structures treat the absence of a device and the misuse of a device as entirely separate violations. If an auditor measures your machine’s stopping time and finds that the ram drifts past the curtain’s trigger point, you are not cited for lacking a guard. You are cited for having a defective safety system. Fines for a botched installation often exceed those for having no guard at all, because a drifting ram suggests negligence masquerading as compliance. The curtain detected the intrusion perfectly. The machine simply failed to respond. Who pays the price when the hardware lies to the operator?
OSHA’s own 1991 interpretation letter explicitly warns that light curtains on press brakes “most always result in limiting the use of the machine.” Shops buy these systems expecting plug-and-play productivity. They quickly discover that a mathematically compliant installation—which requires a calculated minimum setback distance from the tooling—interferes with an operator’s ability to bend small flanges.
Faced with this friction, shops take shortcuts. They move the mounting brackets an inch closer to the die so the operator can hold the part. They blank out the middle beams to accommodate a backgauge. They turn a life-saving device into expensive shop-floor theater.
True compliance is a mathematical anchor, not a fixed checkpoint. A curtain positioned correctly in January based on a new brake’s stopping time can become non-compliant by June because of valve wear, hydraulic fluid degradation, and fixture drift. If you are not measuring that stopping time with an analyzer and adjusting your safe distance accordingly, you do not have a safety system. You have a ticking clock.

A light curtain mounted on a mechanical power press with a full-revolution clutch is explicitly illegal under OSHA 1910.217. The reason is pure physics. Once a full-revolution clutch engages the flywheel, the ram will descend to the bottom of its stroke, no matter how many infrared beams the operator breaks. The machine physically cannot stop. This extreme example reveals the core truth of all press brake safety: the sensor does not protect the operator. The machine’s braking mechanism does.
The manufacturer’s box advertises a “14-millisecond response time.” Shop owners read that number, assume the system is instantaneous, and bolt the brackets right next to the tooling. But those 14 milliseconds only represent the time it takes for the light curtain’s internal solid-state relay to drop the signal. That figure ignores the heavy lifting required by the rest of the machine.
Electrical signals must travel to the machine control, which then de-energizes the hydraulic valves. The hydraulic fluid must bypass, and the massive steel ram—carrying tons of downward kinetic energy—must physically stop its momentum. That mechanical sequence takes time. If your press brake takes 250 milliseconds to halt the ram, your total stopping time is 264 milliseconds. At the OSHA-mandated hand-speed constant of 63 inches per second, an operator’s hand travels more than 16 inches in that quarter-second. If your curtain is mounted four inches away, the operator’s fingers are crushed before the hydraulics even begin to react.
Machine reaction time is also entirely variable. A cold press brake on a Monday morning stops faster than a hot one running at full capacity on a Friday afternoon. As hydraulic oil heats up, its viscosity drops. Thinner oil leaks past worn valve seals faster, adding precious milliseconds to the stopping time. If you calculate your safe distance using a factory-spec response time instead of measuring the machine’s actual stopping time under worst-case thermal conditions, your safety margin is a fiction.
OSHA 1910.217 provides the baseline regulatory formula for safe distance: multiply the hand-speed constant (63 inches per second) by the machine’s total stopping time. If you stop there, you will fail an audit and could lose a finger.
Press brakes operate differently from standard mechanical power presses, which is why compliance auditors immediately look to ANSI B11.3. The ANSI standard introduces a critical variable that OSHA’s baseline formula omits: the depth penetration factor (Dpf). Light curtains are manufactured with different beam resolutions. A 14mm resolution curtain is tight enough to detect a finger, but a 30mm resolution curtain has gaps wide enough that an operator’s hand can slip partially through the sensing field before breaking a beam.
ANSI requires you to add this physical penetration depth to your OSHA baseline calculation. If you use a 30 mm curtain, the calculation requires you to place the mounting brackets several inches farther from the pinch point to account for the distance the hand travels before the sensor detects it. You cannot simply look at the OSHA baseline and start drilling tapped holes. The combined formula is not a best practice; it is the exact mathematical threshold between a near miss and an amputation.
OSHA’s 1991 standard interpretation letter acknowledges a quiet, frustrating truth about the industry: light curtains on press brakes “most always result in limiting the use of the machine.”
Apply the calculation we just established. If your stopping time and penetration factor dictate a safe distance of 18 inches, the light curtain must be positioned 18 inches from the die. Now watch an operator try to bend a 3-inch flange on a flimsy piece of 20-gauge steel. They physically cannot support the material without reaching their arms through the light curtain, breaking the beam, and stopping the machine. The calculation ensures safety, but it destroys the process.
This is where the shop floor clashes with the safety manual. When the calculated distance makes the job impossible, the operator does not stop working. They adapt. They mute the curtain, program a floating blanking window that is dangerously large, or physically unbolt the brackets and slide them closer to the die. The mathematical anchor holds, but the human element snaps. How do you engineer a system that respects the unyielding physics of stopping time without forcing the operator to cheat just to meet their production quota?
Operators cheat the calculation because it pushes them too far back to do their jobs. The industry’s answer to this ergonomic problem is often to abandon traditional light curtains entirely. OSHA explicitly permits close-proximity laser safeguarding systems, such as AKAS or LazerSafe, on hydraulic press brakes under 1910.212; these ride just millimeters below the punch and allow the operator to hold the sheet metal during the bend. But moving the sensor closer to the pinch point removes your mechanical margin of error. You are now relying entirely on the electrical integration between that sensor and the hydraulic valves to protect the operator’s hands.
I routinely audit shops that spend $8,000 on a state-of-the-art laser system to solve their bending clearance issues, only to wire the receiver directly into a single $15 general-purpose relay on an aging hydraulic brake. They assume the expensive sensor guarantees safety. It does not. If that single relay fails, the sensor’s signal disappears into a dead circuit, and the ram crushes whatever is on the die.
Category 3 and Category 4 control architectures exist to eliminate exactly this scenario. A Category 3 system provides redundancy: it uses two separate electrical channels to send the stop signal. If one channel fails, the other still drops out the hydraulic valves. Category 4 goes further by adding continuous monitoring: the system actively checks both channels for faults before every single stroke. While some shops argue that hydraulic press brakes covered by OSHA’s looser 1910.212 standard do not strictly require Category 4 wiring, ANSI B11.3 requires true control reliability. Specifically, ANSI B11.3 requires the safety-related parts of the control system to meet ISO 13849-1 Performance Level ‘e’ (PLe) for high-risk pinch points, legally binding you to that Category 4 architecture. If a single component failure can prevent the machine from stopping, your safety device is just expensive shop decoration.
A forklift strikes a section of rigid conduit on the shop floor, cleanly severing the return signal wire from the light curtain receiver to the main control cabinet. The operator, unaware of the damage, presses the foot pedal. What happens next depends entirely on whether your electrical integration was designed to be fail-safe.
Standard industrial wiring often relies on “normally open” circuits, where a switch sends a voltage pulse to trigger an action. If you wire a safety sensor this way, the machine waits for a positive signal to initiate an emergency stop. When the forklift severs that wire, the stop signal can never reach the controller. The operator breaks the invisible beam, the sensor calls for the machine to halt, but the severed wire means the hydraulic valves remain energized. The ram keeps descending.
True control reliability reverses this logic. Safety circuits must be wired “normally closed,” meaning the sensor continuously feeds a 24-volt signal to the machine control simply to keep it running. The absence of that signal—whether caused by a hand breaking the beam, a power outage, or a forklift severing a conduit—immediately de-energizes the circuit and stops the ram. You must engineer the system so that gravity and loss of electrical power always default to a stopped machine.
Every time a mechanical relay opens and closes to stop a hydraulic valve, a microscopic electrical arc jumps across the contacts. Over 100,000 cycles, that intense heat pits and melts the metal. Eventually, the contacts weld completely shut.
Redundancy without monitoring creates a deadly, silent trap. Suppose your press brake has a Category 3 setup with two redundant relays. Relay A welds shut on a Tuesday. The operator breaks the light curtain beam, and Relay B successfully stops the machine. The operator notices nothing unusual and keeps working. Your redundant system has just been silently downgraded to a single-point failure system. Three months later, Relay B welds shut. The next time the operator reaches into the die space, the machine does not stop.
Force-guided relays combined with a monitoring circuit are the only way to detect this silent failure. In a force-guided relay, the contacts are mechanically linked. If one contact welds shut, the other contacts are physically held in place and cannot change state. The monitoring circuit detects this mechanical mismatch immediately. It allows Relay B to stop the current stroke, but it absolutely prevents the machine from initiating the next one. You cannot visually inspect a welded relay contact, which means verifying this invisible chain requires a specific sequence of physical, shop-floor tests before the operator ever touches a foot pedal.
Before you drill a single hole for a physical bracket, you have to prove that the electrical chain you just wired actually works. You do this by forcing a failure. Step up to the control cabinet, locate the return signal wire from your newly wired force-guided relays, and pull it off the terminal block mid-stroke. If the ram does not stop instantly, your wiring is wrong. Reconnect it, cycle the machine, and manually jam one of the redundant relays shut with a non-conductive probe. The machine should stop and refuse to reset for the next stroke. Only after passing these brute-force electrical tests do you earn the right to mount the physical hardware.
A perfectly leveled light curtain bracket on a Sunday afternoon means nothing once the shop starts up on Monday morning. I have watched maintenance crews spend hours using laser levels to align emitter and receiver towers to within millimeters, only for the system to throw a nuisance fault the moment a forklift drops a skid of steel two aisles away.
Light curtains depend on a precise optical handshake. If the emitter tower deflects even half a degree, the beam misses the receiver’s photoreceptors. Press brakes generate enormous kinetic energy. When the punch bottoms out in the V-die, that shockwave travels through the machine frame and directly into the mounting brackets. If you use standard L-brackets made from thin-gauge aluminum, they will behave like tuning forks. The vibration is amplified at the top of the towers, breaking the optical plane and stopping the machine for no logical reason.
You must use heavy-duty, gusseted steel brackets isolated with rubber shock mounts. Push hard against the top of the emitter tower with your hand. If you can visibly deflect it, the machine’s vibration will eventually break the beam. When operators get three nuisance faults in an hour because of flimsy brackets, they stop seeing a safety device. They see a broken machine that keeps them from making piece-rate. How do you ensure the machine’s stopping capability does not drift out of specification just as quietly as the brackets vibrate out of alignment?
Brake linings glaze over. Hydraulic oil degrades. Valve spools collect microscopic metal shavings and begin to stick. The 90-millisecond stopping time you measured on installation day will not still be 90 milliseconds six months later.
A stop-time monitor (STM) is the only component that detects this mechanical degradation before it closes the gap between a safe distance and an amputation. You have two integration choices: an external STM bolted to the side of the cabinet, or a system hardwired directly into the machine’s CNC controller. External units use a separate rotary cam or linear encoder to measure ram speed. They are easier to retrofit on older mechanical friction-clutch brakes, but they add another layer of external wiring that can be damaged or bypassed.
Hardwiring the STM into the safety PLC is the better method for modern hydraulic brakes.
The controller already monitors the linear scales that track ram position down to the micron. By integrating the STM software directly into the control architecture, the machine continuously calculates its own stopping performance on every stroke. If the stopping time drifts past the programmed limit by even five milliseconds, the controller locks out the machine. For shops evaluating a modern CNC-based bending platform rather than retrofitting around older controls, ADH Machine Tool’s CNC press brake is a relevant next step because it sits within a broader CNC-focused sheet metal portfolio built around bending and automation. But knowing the machine will stop in time is only half the battle. The other half is knowing exactly when it is permitted to ignore the safety sensor entirely.
Muting is the most dangerous, misunderstood, and heavily abused function on a press brake. OSHA allows the light curtain to be temporarily bypassed—muted—during the final phase of the stroke so the operator can hold the workpiece as it bends upward. The rule is absolute: the muting point must be set no higher than 1/4 inch above the material.
Set it any higher, and you leave enough space for an operator’s finger to slip between the punch and the sheet metal while the safety system is blind. Set it any lower, and the light curtain will fault when the punch reaches the natural wave of a warped sheet. You cannot set this by eyeballing a tape measure while jogging the ram down.
To set this safely, use a precision 1/4-inch gauge block. Place your actual material on the die, set the gauge block on top of it, and lower the ram in slow-speed setup mode until the punch just touches the block. Lock the ram. Then adjust your muting limit switch or CNC parameter so it triggers at this exact position.
Remove the block, cycle the machine, and watch the muting indicator light. It should come on a fraction of a second before the punch contacts the steel. This 1/4-inch threshold is mathematically flawless for safety. But what happens when an operator needs to bend a complex box with pre-formed side flanges that break the light beam long before the punch reaches that ideal muting point?
You are forming a five-inch-deep electrical enclosure. Bends one, two, and three run perfectly. On bend four, the previously formed side flanges point straight up toward the ram. As the tooling descends, those vertical flanges cut right through the light curtain’s optical field long before the punch reaches the 1/4-inch muting threshold. The machine stops. The operator is locked out.
This is not a rare edge case. A 1991 OSHA standard interpretation explicitly warned that practical applications of light curtains on versatile press brakes are rare precisely because complex profiles inevitably block the beam. Press brakes are designed to wrap metal around tooling; light curtains are designed to stop the machine the moment anything enters the plane. The two concepts are fundamentally in conflict.
Operators are paid to produce, not to stand in front of a faulted machine. So they find a workaround. They access the safety controller and program the curtain to ignore the specific photoreceptors blocked by the side flanges. They create a temporary dead zone in the invisible wall. The machine runs, the box gets bent, and the operator makes rate.
They have also created a large, unmonitored window directly in front of the pinch point.
There is a critical legal and physical difference between exact blanking and floating a beam. ANSI B11.3 permits exact blanking, but only under extremely strict conditions. If you have a fixed material support table that permanently blocks two specific beams at the bottom of the curtain, you can program the system to ignore them. This is legal because the physical table completely fills the dead zone. A hand cannot occupy the space where the table already exists.
Floating a beam to clear a box flange violates this basic law of physics.
When an operator programs a floating window to let a piece of 16-gauge sheet metal pass through the curtain, the sheet metal is only 0.060 inches thick. The operator usually disables a two-inch vertical block of beams to account for the material’s movement during the stroke. The metal does not fill that two-inch void. A human hand is roughly 1.5 inches thick across the knuckles. By floating the beam to clear the part, the operator has engineered a custom loophole perfectly sized for their own fingers, exactly where their hands are actively manipulating the material.
Hydraulic press brakes fall under OSHA’s 1910.212 general machine-guarding standard. The standard is performance-based: the guard must prevent hands from entering the danger zone during the operating cycle. When an inspector walks your floor, they will ask the operator to cycle the machine on a box bend. If the inspector can pass a 1.5-inch dowel rod through the light field next to the flange without tripping the brake, they will issue the citation before the shift ends.
Sometimes the light curtain is simply the wrong tool for the job. When a setup requires bending a large, flimsy sheet of 20-gauge steel, the operator has to support the material from underneath to keep it from kinking under its own weight. As the flange folds upward, the operator’s arms naturally rise into the light field; in that case, the safer next step may be choosing equipment built for large-format CNC bending, such as ADH Machine Tool’s large press brake, rather than forcing a safeguard to fit the wrong process.
If the safety system faults during normal material handling, the shop floor will inevitably bypass it.
This is the point where you must walk away from the light curtain entirely. Under 1910.212, a guard that must be disabled to perform normal work is not a compliant guard. If the part profile requires hands to occupy the optical plane, bolting a curtain four inches back from the die is reactive compliance. It is a decoration hung to satisfy an auditor, not a mechanism that saves a hand.
True compliance requires matching the technology to the physics of the bend. If complex profiles dominate your schedule, you must abandon fixed curtains and evaluate safeguards as part of the machine system, not as an accessory. That may mean active laser guarding systems that travel with the ram, monitoring the exact millimeter of space directly below the punch tip, or engineering the hazard out entirely with two-hand controls and a rapid advance that stops dead before the pinch point. For teams comparing press brake options and implementation details, ADH Machine Tool’s R&D focus on press brakes, automation, and intelligent equipment makes its download resources a practical next step before a supplier discussion. The invisible chain of safety cannot have a “sometimes” link.
Whether you rely on a fixed curtain, an active laser, or two-hand controls, every safeguarding technology shares one critical vulnerability: each depends entirely on the press brake’s mechanical ability to stop exactly when commanded. Oil gets hot, sludge builds up in the proportional valves, and O-rings flatten. A machine that stopped in 90 milliseconds on the day the OSHA auditor approved it in January will not stop in 90 milliseconds in July.
The degradation of stopping time is invisible. You cannot hear a hydraulic valve closing ten milliseconds slower than it did yesterday. Because this decay is silent, safety standards require a daily stop-time performance test. But a mandate on paper is useless on the floor if the chain of command is fractured.
So, who holds the stopwatch?
The safety manager wrote the policy, but they are in a budget meeting. The maintenance tech has the tools, but they are buried in a forklift repair. That leaves the operator. The operator must run the daily test. They are the one putting their hands in the die.
But logging the test cannot be a pencil-whipped checkbox on a clipboard hanging beside the controller. If the operator tests the brake and the stop-time monitor flashes 105 milliseconds instead of the 90-millisecond baseline, they need unquestioned authority to lock out the machine. If the operator records the failure but production still forces them to run the job, the safety manager is legally culpable and the operator is physically exposed. The chain breaks.
Suppose the operator does their job. The monitor shows a 15-millisecond drift. The machine is now officially out of compliance.
For teams weighing whether to relocate the guarding or address the stopping system itself, ADH Machine Tool’s CNC-focused portfolio across bending, shearing, laser cutting and sheet-metal automation makes its technical materials a useful next reference; you can download the relevant brochure or specification material before deciding what corrective action to scope.
Fifteen milliseconds is about the time it takes a bee to flap its wings once. It sounds trivial. It is not. At the standard hand-speed constant of 63 inches per second, a 15-millisecond delay means an operator’s hand moves nearly a full inch deeper into the die space before the ram stops. Your safety device—whether it is a fixed curtain, a two-hand console, or an active laser—was mathematically tied to the January stopping time. That anchor has just moved.
You now face a brutal, expensive choice.
Option one: you unbolt the light curtain brackets or the two-hand control pedestal and move them an inch farther away from the pinch point, recalculating the safe distance for the new, slower stopping time. Option two: you lock out the brake, tear down the hydraulic manifold, rebuild the sluggish valves, and restore the machine to its original 90-millisecond baseline.
Moving the brackets is cheap today, but it reduces the operator’s working envelope and slows production. Rebuilding the brake is expensive today, but it treats the disease instead of accommodating the symptom. What you cannot do is ignore it.
The choice between rebuilding a sluggish hydraulic manifold and simply sliding your safety brackets an inch farther back is not a safety decision. It is a production math problem. Accommodating mechanical decay by expanding the safe distance may feel like a free fix that keeps the line moving, but it is really a permanent, compounding tax on your throughput. To stop bleeding cycle time and start guaranteeing safety, you need a ruthless, binary evaluation of your floor. No “maybe,” no “mostly compliant.” Use this framework Monday morning.
When I walk into a shop as an auditor, I do not care how expensive your light curtains are. I look for proof of performance. Run this Go/No-Go audit on every press brake you own. A single “No” means the machine is unsafe to operate.
You cannot overhaul every press brake on the floor by Monday morning. When capital is tight and production schedules are unforgiving, you must triage the invisible chain in this exact order of operations:
Stop treating light curtains as plug-and-play accessories designed to satisfy a regulator. Bolting a pair of yellow optical tubes to the side of a press brake does not make the machine safe. It only creates a tripwire.
What actually stops the ram is the entire integrated system: the unyielding rigidity of the brackets, the redundant architecture of the safety relays, and the immediate response of the hydraulic valves. Your new baseline is simple: own the math, enforce the daily tests, and engineer out the loopholes. If the machine cannot stop fast enough to protect the operator at a distance that still allows efficient production, you do not bypass the sensor—you fix the machine.
For teams evaluating practical options here, Tandem Press Brake is a relevant next step.
